Under laboratory conditions, one optical fiber can carry over 100 terabits per second. This capability is rooted in the precision of the cable’s construction. For manufacturers, the FTTH Cable Production Line serves as the cornerstone for delivering reliable broadband, wireless networks, local-area networks, and data transmission.
Fiber Secondary Coating Line

Fiber Secondary Coating Line

Compact Fiber Unit
This integrated system encompasses various stages, including fiber coloring, secondary coating, tight buffering, SZ stranding, extrusion, armoring, sheathing, tape wrapping, cooling, curing, and optical and mechanical testing. These processes collectively transform raw fiber into cables suitable for complex network installations.
Contemporary fiber optic cable manufacturing equipment can be tailored for FTTH drop cables, indoor cables, outdoor loose-tube designs, armored cables, and ribbon-based products. Some machines also cater to specific high-density datacom designs.
The design of the production line is contingent upon the cable’s structure, fiber count, materials, production capacity, adherence to product standards, and the available factory space. Advanced systems can handle both single-mode and multimode fiber, including ITU-T G.652D and bend-insensitive G.657A1 and G.657A2 fiber.
This article examines the components, process options, automation, testing, installation, and long-term efficiency required for high-speed fiber cable production in the United States. It also explores how an adaptable FTTH cable manufacturing system can accommodate evolving market demands.
Main Points
- An FTTH Cable Production Line integrates multiple cable-making processes into a unified system.
- Manufacturers can configure equipment for various cable types, including indoor, outdoor, armored, drop, and ribbon cables.
- The choice of fiber type, cable structure, materials, and factory layout influences equipment selection.
- Process control and testing help preserve optical performance and reduce manufacturing waste.
- Scalable machinery supports high-speed production and future cable variations.
What Is An FTTH Cable Production Line?
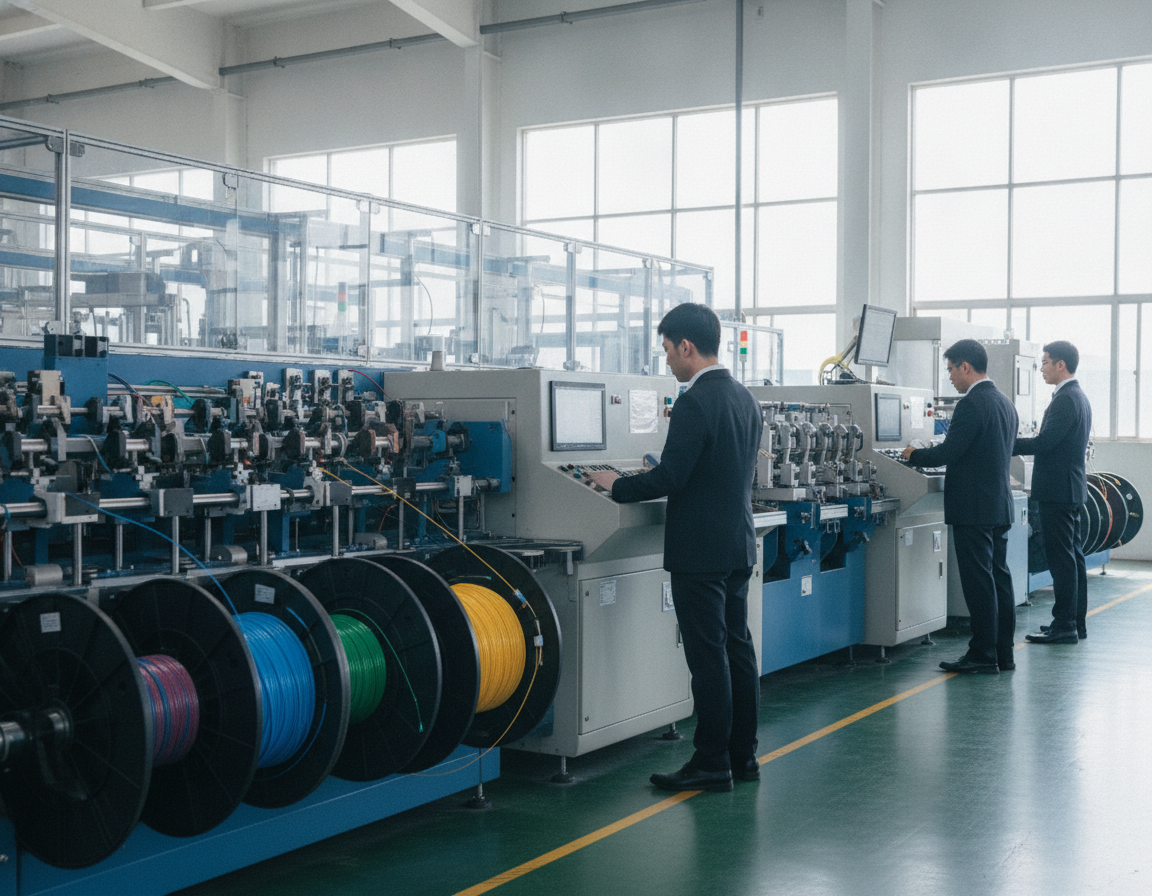 FTTH Cable Production Line
An FTTH cable manufacturing line constitutes a sophisticated ensemble of machinery, transforming raw materials into sophisticated fiber-to-the-home cables. This process meticulously controls fiber tension, coating thickness, and cable geometry, ensuring precise material placement at each stage.
Communication and computer networks depend on cables with consistent dimensions and accurately positioned fibers. The production line integrates various systems, including fiber payoff, coloring, buffering, stranding, extrusion, cooling, testing, and take-up, within a unified, controlled framework.
The Purpose Of An FTTH Cable Manufacturing System
The main purpose of this system is to protect delicate glass fibers while preserving their optical performance. By regulating tension, it prevents stress during the manufacturing process. The application of a consistent coating and precise jacket geometry facilitates smooth installation and ensures long-term signal transmission fidelity.
Contemporary FTTH drop cable production lines are capable of producing a variety of cable types, including flat and round drop cables, simplex, duplex soft cables, and tight-buffered cables. These systems offer flexibility, allowing manufacturers to customize production based on fiber count, jacket materials, strength members, and final diameters.
Typical FTTH Cable Structures And Applications
Indoor fiber optic cable lines cater to a range of applications, from premises wiring to FTTA and FTTB deployments, local-area networks, patching environments, and building distribution. The common configurations include GJFJV, GJFV, simplex, duplex, and tight-buffered cables, each tailored for specific indoor use cases.
Outdoor networks, on the other hand, demand strong protection against environmental factors such as moisture, pulling force, crushing, temperature fluctuations, and ultraviolet radiation. The manufacturing of outdoor cables encompasses a variety of designs, including ADSS, ASU, GYXTC8S, GYXTPY, GYXTW, armored, loose-tube, aerial, duct, and direct-buried cables, each designed for specific outdoor applications.
Different cable structures are intended for particular installation conditions. Tight-buffered cables are ideal for indoor handling, while loose-tube designs accommodate fiber movement due to temperature variations. Armored cables, with their added protection, are suited for challenging routes.
The Effect Of Production Quality On Network Performance
Fiber cable quality directly affects attenuation, tensile strength, crush resistance, bending performance, and environmental durability. Inadequate fiber positioning or uneven coating can significantly increase signal loss. Weak jackets, conversely, may lead to damage during handling, bending, or installation.
Quality control measures, including dimensional checks, tension monitoring, optical measurements, and mechanical tests, are integral to maintaining consistent output. Standards like IEC 60794 provide critical benchmarks for cable performance. ITU-T G.652D and G.657A1/A2 guidelines further specify fiber characteristics for standard, bend-sensitive, and access network applications.
Consistent manufacturing processes enhance installation efficiency and ensure stable service over the cable’s lifespan. For network operators, the reliability of production directly correlates with reduced field issues, expedited deployment, and dependable high-speed connectivity.
Essential Modules In Fiber Optic Cable Manufacturing Equipment
Each production stage is designed to safeguard the fiber and manage its positioning. The process ensures accurate payout, alignment, and tension, preventing bends, scratches, and signal loss. These steps are critical in preparing the fiber for the subsequent cable assembly stages.
Fiber Preparation And Coloring Equipment
Fiber preparation begins by guiding each strand from the payoff reel while maintaining accurate tension control. Alignment systems are integral in maintaining the fiber’s central position as it traverses the manufacturing line. Surface protection mechanisms are implemented to minimize damage during the coloring, buffering, and cable assembly processes.
A dedicated fiber coloring machine applies separate color coatings to individual strands. These colors are essential for quick identification during the assembly and field termination phases. Some systems boast up to 12 coloring channels and UV curing speeds exceeding 1,500 meters per minute.
A fiber draw tower creates optical fiber from glass preforms. While it plays a significant role in broader fiber manufacturing operations, most FTTH cable lines utilize pre-manufactured optical fiber.
Secondary Coating And Buffering Equipment
A secondary coating line creates loose tubes around one or more fibers using dry materials or a jelly-filled compound. This protective layer adds space, enhances protection, and allows for the fiber’s free movement within the cable.
The OFC 40 Secondary Coating Line is designed for high-speed production, ensuring stable excess fiber length and consistent tube quality. These features are vital in maintaining cable dimensions during subsequent stranding and sheathing processes.
Tight-buffering machinery places a close-fitting polymer layer around the fiber, making it suitable for indoor cables requiring easy handling and direct termination. The choice of buffer type is contingent upon the cable’s structure, installation requirements, and necessary protection levels.
Stranding, Extrusion, And Sheathing Units
Stranding machinery organizes tubes, ribbons, or other elements around the core while controlling lay length and core shape. This process ensures stable cable geometry during pulling and installation, critical for maintaining performance.
Extrusion and sheathing units place protective jackets on cables intended for indoor or outdoor use. Common materials include PE, PVC, and LSZH. Temperature, pressure, and cooling control are essential in producing a smooth, accurately dimensioned jacket.
Complete optical fiber cable making machines may include steel tape or wire armoring units. Yarn application, tape wrapping, and cable testing are integral components of these lines. These modules enable manufacturers to tailor protection levels to various applications, including aerial, buried, indoor, and direct-burial installations.
| Module |
Main Function |
Typical Production Value |
| Fiber preparation |
Manages payout, alignment, tension, and fiber surface protection |
Reduces fiber damage before cable assembly |
| Fiber color-coding machine |
Adds color coatings to identify individual fibers |
Supports up to 12 channels and UV curing above 1,500 meters per minute |
| Optical fiber draw tower |
Draws optical fiber from preforms |
Used in fiber manufacturing operations, not most FTTH cable lines |
| Fiber secondary coating line |
Creates dry or jelly-filled loose tubes |
Maintains excess fiber length and consistent tube dimensions |
| Tight-buffering unit |
Places a close-fitting polymer layer around the fiber |
Helps produce compact indoor cables |
| Stranding unit |
Arranges tubes, ribbons, and cable elements around the core |
Supports controlled lay length and stable cable shape |
| Extrusion and sheathing unit |
Places PE, PVC, or LSZH protective jackets |
Protects cables used in indoor and outdoor installations |
| Armoring and testing modules |
Provides steel armor, yarn, tape, and testing functions |
Builds cables for demanding routes and verified quality |
Configuration Choices For An FTTH Cable Production Line
Fiber cable plants can be tailored for one product or multiple cable families. The optimal setup hinges on cable structure, fiber count, materials, production speed, and testing requirements. A modular design facilitates manufacturers in balancing output, floor space, and future growth prospects.
Drop Cable And Indoor Cable Configurations
A typical FTTH drop cable production line integrates fiber payout, coloring or identification, strength-member handling, extrusion, cooling, take-up, and inline inspection. This sequence ensures stable dimensions and precise fiber placement. It accommodates common drop cable designs for residential, commercial, and access networks.
An indoor cable production line caters to simplex, duplex, GJFV, GJFJV, tight-buffered, premises, and soft cable types. It employs aramid yarn, fiberglass rods, or other strength members. Material selection is contingent upon bend performance, pulling force, flame behavior, and installation conditions.
The OFC 43 Premises Cable Extrusion Line is suitable for indoor and FTTH cable designs. Its process encompasses stranding, yarn application, and extrusion. This adaptable layout enables a plant to transition between small premises cables and selected access cable designs with minimal production adjustments.
Outdoor Loose-Tube And Armored Cable Options
Outdoor fiber optic cable production begins with secondary coating. The process then involves SZ stranding, strength-member application, water-blocking materials when necessary, and final jacketing. These steps safeguard fibers against moisture, tension, temperature fluctuations, and movement during installation.
The OFC 40, OFC 70, and OFC 60 process sequence comprises three primary stages: loose-tube production, SZ stranding, and final cable jacketing. Each stage is customizable to match the target core count, tube design, cable diameter, and jacket material. Inline controls ensure consistent tube size and cable geometry across extended production runs.
Armored cables use steel tape or steel wire wrapping to provide greater mechanical protection. Adjustable tension prevents gaps, deformation, and excessive pressure on the cable core. This configuration is suitable for direct-burial, duct, industrial, and other demanding outdoor applications.
Customized Production Lines For Cable Requirements
Custom line design starts with a review of the product drawing. Engineers scrutinize core count, fiber type, cable diameter, sheath material, production speed, quality standards, and plant layout. This review determines the necessary payoffs, extruders, stranders, cooling systems, take-ups, and inspection devices.
Manufacturers can opt for individual process modules or a complete turnkey fiber optic cable production line. A plant may require one extrusion unit for a focused product range. Larger facilities might integrate coloring, buffering, stranding, armoring, jacketing, and testing equipment.
An advanced FTTH cable extrusion line can support newer materials, closer tolerances, and quicker changeovers. Existing lines can be upgraded with newer controls, improved cooling, modern inspection tools, or efficient drives. These enhancements extend service life, boost productivity, and maintain competitiveness.
Project teams seeking high-quality FTTH cable production solutions should evaluate output targets against product variety and available floor space. A well-matched configuration minimizes material waste and ensures stable, repeatable production.
| Configuration |
Main Process Modules |
Typical Cable Uses |
Main Design Priority |
| FTTH drop cable |
Fiber payout, identification, strength-member handling, extrusion, cooling, take-up, and inline inspection |
FTTH access drops and short subscriber links |
Small diameter, bend performance, accurate fiber placement |
| Indoor cable |
Fiber payout, tight buffering, yarn application, extrusion, cooling, and take-up |
Simplex, duplex, GJFV, GJFJV, premises, soft, and tight-buffered cables |
Flexibility, flame performance, low installation force |
| Outdoor loose-tube cable |
Secondary coating, SZ stranding, strength-member application, water blocking, and jacketing |
Duct, aerial, direct-burial, and access network cables |
Moisture resistance, tensile strength, temperature stability |
| Armored fiber cable |
Loose-tube or stranded core, steel tape or wire wrapping, final jacketing |
Industrial, direct-burial, and high-protection installations |
Adjustable armor tension and mechanical protection |
| Custom turnkey line |
Selected modules or a complete integrated production system |
Special cable designs and mixed product portfolios |
Product drawings, speed, standards, layout, and upgrade path |
Fiber Coloring, Secondary Coating, And Tight Buffering Processes
Fiber processing begins with bare fiber or fiber that already has a 250 µm primary coating. A specialized fiber coloring machine then applies a precise, thin layer to each fiber within a multi-fiber cable. This meticulous process ensures swift identification during the subsequent splicing and installation phases.
Contemporary coloring technologies are capable of processing up to 12 channels concurrently. Utilizing UV curing equipment, the color layer is solidified at velocities exceeding 1,500 meters per minute. Ensuring stable fiber tension, uniform ink flow, and consistent curing processes are imperative to avert irregular coloration, surface imperfections, and damage to the fiber.
Following the coloring phase, a secondary coating line envelops one or more fibers within a protective sheath. This line can generate either dry loose tubes or jelly-filled counterparts. Each configuration necessitates a stable excess fiber length, accommodating variations in temperature and mechanical stress.
The dimensions of the tube must remain invariant throughout the extrusion, cooling, and post-shrinkage phases. Maintaining a consistent tube profile is critical for preserving the cable’s geometry and mitigating stress on the optical fiber. Achieving precise material flow and controlled cooling is essential to minimize dimensional discrepancies across extended production periods.
Tight buffering is an important process for producing indoor and FTTH cables. It encompasses the formation of tight-buffered fibers, semi-tight buffers, and micro-sheath products. Hytrel, PVC, and LSZH are commonly employed as buffer materials, with tight-buffer layers produced within a 600–900 µm extrusion range.
Water troughs cool the newly formed buffer layer and remove excess heat. Subsequent UV drying or curing may be necessary, contingent upon the material system’s requirements. These steps are critical for stabilizing the final profile and facilitating clean winding, connector preparation, and cable assembly.
Process control integrates fiber tension, material temperature, die alignment, curing conditions, and take-up speed. Operators meticulously monitor these parameters to minimize the occurrence of bubbles, ovality, surface defects, and excess scrap. Achieving a harmonious process balance is essential for safeguarding the fiber while maintaining the cable’s optical integrity.
SZ Stranding Line Technology For FTTH And Outdoor Cables
An SZ stranding line envelops central cores with tubes, ribbons, or other cable elements, altering lay directions at predetermined intervals. This method facilitates the creation of flexible cable geometries and controlled core formations.
Alternating lay directions allow fibers to move within the cable. This movement aids in managing strain during bending, pulling, and temperature fluctuations. Such a technique is predominantly employed for outdoor applications and in the production of dense fiber cable cores.
The SZ Stranding Process
During SZ stranding, payout units guide tubes or ribbons toward a central strength member. The stranding head, rotating around the core, changes direction at intervals determined by the lay length. A binding unit secures the elements in place before they reach the take-up system.
The OFC 70 SZ-Stranding Line is designed to strand different cable elements at high speeds. It supports controlled lay lengths, precise binding, and accommodates long production batches. Depending on the configuration, it can handle up to 24 fibers, with rotation speeds reaching 3,000 rpm.
Advantages Of Servo-Controlled Stranding
Servo-controlled stranding ensures synchronization among payout, rotation, binding, and take-up systems. Each servo motor adjusts to production settings in real-time. This synchronization enhances lay-length accuracy and maintains consistent binding tension.
Consistent synchronization supports uniform cable diameter and helps reduce fiber stress. It facilitates smoother handling during extrusion and sheathing processes. The consistent core geometry ensures reliable optical performance across extended production runs.
- Precise lay length for stable core construction
- Balanced tension across tubes and ribbons
- Coordinated take-up for smooth, continuous production
- Reduced risk of unwanted fiber movement and strain
- Better process control for high-speed fiber cable production
When To Use SZ Stranding In An FTTH Facility
SZ stranding suits outdoor loose-tube cables, ribbon-based designs, and cable cores containing many organized elements. It offers manufacturers a flexible platform for producing high-count products, trunk cables, and network cables for challenging routes.
A facility producing only basic FTTH drop cables may not need a complete SZ stranding line. Diversified plants, on the other hand, can use the equipment for expansion into outdoor cables, high-density products, and longer production batches.
SZ super-bundling is a related process for combining rollable ribbon bundles into structured super bundles. These bundles are suitable for compact datacenter interconnect cables, where fiber density, flexibility, and organized routing are critical.
Fiber Cable Extrusion And Sheathing For FTTH Protection
Extrusion applies an outer jacket to the fiber cable, helping protect it from moisture, abrasion, and other environmental conditions. The jacket must endure exposure to sunlight, temperature fluctuations, and other outdoor elements. A well-controlled extrusion process ensures the cable’s performance remains stable from the manufacturing stage to its deployment.
Jacket Materials Used For Indoor And Outdoor Cables
Polyethylene (PE) is commonly selected for outdoor jackets because it resists water and weather conditions. This makes PE fiber cable jackets ideal for direct burial, aerial, and duct applications. The material can be customized for enhanced flexibility, strength, and environmental resilience.
PVC and LSZH are commonly used for indoor cable designs. PVC supports durable jackets and buffer layers, suitable for general building applications. LSZH fiber cable production is preferred where low smoke and reduced halogen emissions are critical during fires.
Hytrel is utilized in tight-buffer applications requiring flexibility and dependable recovery. PVC and LSZH can also serve as buffer or jacket materials, depending on the cable’s structure. The OFC 60 Jacketing Line is designed for the final outdoor protection and flexible cable designs. It operates at a sheathing speed of approximately 60–90 meters per minute, contingent on cable diameter, material, and configuration.
Cooling, Curing, And Dimension Control
After the polymer exits the die, cooling troughs are used to stabilize the extruded profile. Maintaining consistent water temperature, flow rate, and contact time is essential. These factors are critical in preserving the jacket’s diameter and minimizing surface defects.
UV dryers or curing systems may support compatible coating and marking processes. Integrating energy-saving extrusion and UV-curing technologies can significantly reduce operating costs. A well-controlled line ensures high output without compromising the fiber core.
An advanced FTTH cable extrusion line uses sensors and control systems to regulate important process points. Parameters such as die centering, melt temperature, extrusion pressure, line speed, cooling-water stability, jacket concentricity, and take-up tension all impact cable quality. Even minor adjustments in these settings can affect wall thickness and cable flexibility.
Fiber Cable Sheathing Line Performance Factors
A fiber cable sheathing line must align with the planned cable range, polymer types, and target output. The design of the screw, crosshead accuracy, cooling length, haul-off control, and take-up capacity all influence stable production. The line should facilitate quick size changes, accommodating multiple FTTH cable designs in a factory setting.
Every jacket should be checked for diameter, ovality, surface finish, adhesion, tensile strength, and elongation. Environmental tests assess resistance to heat, moisture, chemicals, sunlight, and repeated bending. These evaluations confirm the jacket’s effectiveness in protecting the cable during installation and service.
- Outdoor cable designs commonly use PE for protection against moisture and weather.
- Indoor designs may use PVC for general durability and flexible processing.
- LSZH materials are suitable where smoke and halogen limits are strict.
- Hytrel may be used in tight-buffer cables that need flexibility and recovery.
- Servo-controlled take-up systems help maintain consistent tension and cable diameter.
| Application |
Typical Material |
Main Protection Need |
Key Process Checks |
| Outdoor FTTH fiber cable |
PE |
Moisture, sunlight, abrasion, and temperature changes |
Wall thickness, concentricity, cooling stability, and jacket finish |
| Indoor distribution cable |
PVC |
Flexibility, abrasion protection, and simple installation |
Diameter, ovality, tensile strength, and take-up tension |
| Low-smoke indoor fiber cable |
Low-smoke zero-halogen material |
Reduced smoke and halogen emissions during fire |
Melt control, surface quality, elongation, and flame-related testing |
| Tight-buffer cable |
Hytrel, PVC, or LSZH |
Flexibility, fiber protection, and predictable stripping |
Buffer fit, adhesion, recovery, diameter, and bending checks |
Fiber Ribbon Line And Compact Fiber Unit Solutions
Ribbon production involves arranging multiple optical fibers in a flat, ordered structure. This method increases fiber density and facilitates rapid mass splicing in high-count cables. It is ideal for datacenter links, central-tube cables, and other space-constrained networks.
Ribbon-Based Cable Production
The OFC 45 Ribbon Buffering Line generates dry and jelly-filled ribbon tubes. These tubes are designed for central-tube and ribbon-based loose-tube cable structures. Controlled buffering safeguards the fibers while maintaining the tube’s compactness, preparing it for subsequent stranding or jacketing.
Rollable ribbon production supports newer high-density datacom systems. The OFC 23 Rollable Ribbon Line creates high-density rollable ribbons for datacenter cable designs. Their flexible nature allows for increased fiber density within a limited cable diameter.
The OFC 79 Rollable Ribbon Bundling Line assembles these ribbons into compact, cable-ready bundles. The OFC 70 SZ Super-Bundling Line then combines these bundles into structured super bundles for datacenter interconnect cable cores. An OFC 60 Jacketing Line can apply the final jacketing.
Fiber Ribbon And “Fiber Ribbone Line” Search Terminology
Fiber ribbone line is often used as a spelling variation for fiber ribbon line. Despite the spelling variation, the technical process remains focused on ribbon production, buffering, bundling, or tube formation. The essence lies in the process control, not the spelling used in product searches.
Integrating Compact Fiber Units
A compact fiber unit integrates one or more fibers, ribbons, strength members, and protective layers into a single, small subassembly. This format supports modular production and space-efficient cable designs. It enables a higher fiber count within restricted cable dimensions.
Compact units are integral to high-density datacom cable manufacturing plans, accommodating flexible product layouts. They can navigate through subsequent bundling, stranding, and jacketing stages with minimal adjustments to the main line. This approach facilitates the production of specialized designs without significantly increasing floor space requirements.
Automation, Testing, And Quality Control In Production
Reliable cable production requires dependable process controls, accurate test data, and rapid fault detection. A contemporary PLC fiber cable production line integrates each phase, from fiber payout to the final cable take-up. This configuration ensures consistent output over extended periods and facilitates uninterrupted operation around the clock.
PLC And HMI Control Systems
The integration of a Siemens PLC and HMI system orchestrates the entire process, from payout to take-up. It synchronizes line speed and material flow across all units, ensuring a seamless operation. The HMI interface empowers operators to access recipes, review alarm histories, monitor process values, and initiate emergency stops.
Accurate fiber path alignment is critical to safeguard the glass during its journey through the production line. Maintaining stable tension is equally important to prevent excessive attenuation, microbending, fiber breaks, and irregular cable geometry. The system allows for the saving of settings for various cable designs, including drop, indoor, and outdoor cables.
Optical And Mechanical Testing Of Cables
Optical fiber cable testing encompasses assessments of attenuation and continuity, as well as transmission performance and fiber identification. These evaluations confirm that each fiber adheres to the specified path and meets performance criteria. Automated testing records are linked to production batches, providing a clear audit trail.
A dedicated testing station may assess optical attenuation, tensile strength, crush resistance, and aging. Mechanical inspections cover tensile strength, crush resistance, heat aging, jacket condition, and dimensional accuracy. The selection of tests must align with the cable’s structure, jacket material, strength member, and intended installation environment.
Quality control begins with the inspection of incoming optical fibers, polymer compounds, and strength members. It extends to the evaluation of finished cable dimensions, optical performance, jacket condition, and production records. Continuous monitoring alerts operators to any deviations from set limits, enabling prompt corrective actions.
Relevant Fiber And Cable Standards
IEC 60794 is an important reference for optical fiber cable specifications. Fiber characteristics may adhere to ITU-T G.652D for standard single-mode designs or ITU-T G.657A1 or ITU-T G.657A2 for bend-insensitive applications. The chosen fiber class must align with the cable’s structure and the network’s requirements.
Documentation may reference ISO 9001 quality systems, CE marking, and RoHS compliance. These references underscore the commitment to traceable production practices and responsible material selection. The test plan should reflect customer specifications, local regulations, and the cable’s intended use.
| Control Area |
Key Functions |
Quality Value |
| PLC And HMI Systems |
Line coordination, recipes, alarms, emergency stops, and process monitoring |
Consistent operation and repeatable production settings |
| Fiber Handling |
Path alignment, payout control, and tension regulation |
Lower risk of attenuation, microbending, and fiber breaks |
| Optical Performance Testing |
Attenuation, continuity, transmission, and fiber identification testing |
Confirmed optical performance |
| Mechanical Performance Testing |
Tensile, crush, aging, jacket, and dimensional inspections |
Improved durability and cable consistency |
| Standards And Compliance Control |
References to IEC 60794, ITU-T G.652D, ITU-T G.657A1, and ITU-T G.657A2 |
Defined design and compliance objectives |
How To Select Efficient Fiber Optic Cable Production Machinery
Initiate the selection process by examining the cable portfolio, not merely the machine list. Determine the plant’s production scope, encompassing various cable types such as drop, indoor, outdoor, and others. This approach ensures that the FTTH cable equipment selection is precise, avoiding costly production capability gaps.
Production Capacity And Line Speed
Match production output to expected demand, treating line speed as one part of the overall assessment. Coating and extrusion units can achieve speeds up to 1,000 meters per minute. In contrast, sheathing lines operate at approximately 60–90 meters per minute. The overall line output is determined by the slowest process, changeover time, and reel handling efficiency.
Assess fiber count, core diameter, cable diameter, lay length, material flow, take-up reel size, and setup time. High-speed fiber cable production lines must maintain consistent tension across all speeds. Request test data specific to the cable designs intended for the plant.
| Assessment Area |
Reason It Matters |
Information To Check |
| Line Speed |
Sets daily output and process balance |
Rated speed, normal operating speed, and loaded speed |
| Fiber Handling Capacity |
Supports existing and future cable products |
Core count, fiber type, and allowable diameter |
| Changeover Time |
Affects small-batch production |
Tool replacement, recipe storage, and reel-changing procedures |
| Material Processing Capacity |
Affects jacket and buffer consistency |
Resin flow, cooling requirements, and material waste |
Materials, Cable Range, And Future Upgrades
Confirm that the optical fiber cable-making machinery supports both single-mode and multimode fibers. The system should accommodate various fiber types, including G.652D and G.657A1/A2. Verify compatibility with materials such as Hytrel, PVC, LSZH, PE, steel tape, and wire armor.
A modular cable production line may combine processes such as fiber coloring, OFC 40 secondary coating, and OFC 60 jacketing. Request customization based on product drawings, core count, target speed, sheath materials, and required standards.
Modular equipment makes later expansion easier. Adding new buffering, stranding, or jacketing units can extend the life of existing equipment. This flexibility supports adapting to changing orders without replacing the entire fiber optic cable line.
Factory Space, Energy Consumption, And Maintenance
Inspect the facility before making a purchase. Many systems require a 380 V AC ±10%, three-phase industrial supply. Power consumption may approach about 55 kW, depending on the configuration. Confirm the necessary floor space, material flow, reel movement, ventilation, cooling water, operator access, safety clearances, and expansion space.
Compare energy-saving extrusion units with UV-curing systems to match the planned products. Review preventive maintenance tasks, cleaning needs, spare-parts access, and service clearance around each module. Clear records and easy access are essential for maintaining the productivity of optical fiber cable-making machines during extended production periods.
A well-planned purchase integrates capacity, materials, layout, energy use, and service support. These considerations form a solid foundation for reliable FTTH production, avoiding unnecessary expenses on unused speed or features.
Installation, Training, And Support For FTTH Cable Manufacturing
The foundation of dependable FTTH cable line installation lies in a meticulously crafted factory plan. Suppliers must meticulously assess the floor area, production flow, access routes, and safety zones prior to equipment delivery. This foundational plan dictates the precise positioning of equipment, ensuring seamless coordination with utilities, line assembly, and cable routing.
Commissioning includes essential steps such as power checks, air and water connections, control-system setup, and process calibration. Engineers are dispatched upon equipment arrival, aligning with the equipment’s complexity, site readiness, and customer needs. Initial production verification is imperative to validate output quality before transitioning to regular operations.
Selecting a turnkey cable production system involves more than receiving machinery. It includes layout design, installation support, operator training, and detailed technical documentation. These documents are indispensable, detailing machine settings, wiring diagrams, operational procedures, maintenance tasks, and safety protocols. Such documentation is instrumental in minimizing downtime and ensuring efficient production management.
Good training for fiber optic cable machinery should combine technical instruction with hands-on practice. Operators must be proficient in handling fibers, loading materials, setting recipes, adjusting tension, and conducting extrusion, stranding, and cable testing. Training should also encompass routine cleaning, safe operation, alarm monitoring, and basic troubleshooting techniques.
Training modalities can vary, with on-site sessions providing hands-on experience and remote sessions facilitating review of control screens, recipes, and standard operating procedures. This dual approach ensures that operators are well-prepared to handle the complexities of the equipment.
- Verify fiber routing, tension control, and material feed settings.
- Review extrusion temperature, line speed, cooling, and jacket dimensions.
- Inspect stranding settings, test results, and production records.
- Train operators in safe shutdown, cleaning, inspection, and fault recovery.
Remote technical support can assist with software settings, program faults, sensor alarms, and equipment problems. A dedicated service team can review operational data, guide diagnostic procedures, and provide replacement support when necessary. Timely response is critical, given the operational demands of a production line serving active customer orders.
Preventive maintenance is essential, encompassing cleaning, lubrication, electrical inspections, calibration checks, and wear-part reviews. Modular equipment typically follows a maintenance cycle of approximately six months. The actual interval, influenced by operating hours, materials, dust levels, line speed, and site conditions, should be clearly outlined in a service plan.
| Support Area |
What To Confirm Before Purchase |
| After-Sales Response |
Support hours, response targets, escalation procedures, and communication methods |
| Replacement Parts |
Stock location, delivery times, compatible parts, and replacement instructions |
| Software Support |
Program backups, updates, access rights, and remote diagnostic options |
| Warranty |
Coverage period, excluded items, labor terms, and claim process |
| Regional Service |
Regional engineers, travel assistance, and available maintenance coverage |
Platforms like Made-in-China.com Secured Trading offer additional security features, including payment protection, shipment tracking, optional pre-shipment inspections, and dispute resolution assistance. It is imperative to confirm details such as freight costs, delivery dates, warranty coverage, and service conditions directly with the chosen supplier.
Advantages Of Modern FTTH Cable Manufacturing Technology
Modern production systems enable cable manufacturers to exert precise control from the initial fiber pay-off to the final jacketing stage. The integration of automated tension control, synchronized drives, stable extrusion, controlled curing, and precise stranding ensures the maintenance of cable dimensions and optical performance. This level of precision is critical for the production of advanced FTTH cables, catering to the demands of complex network projects.
Consistent Cable Quality And Lower Production Waste
Precise process control helps maintain stable excess fiber length throughout cable production. This control supports controlled post-shrinkage, accurate lay length, precise binding, and repeatable jacket dimensions. Such factors are essential in reducing stress on the fiber, ultimately protecting signal quality during both installation and service.
Stable line control can reduce fiber breaks, material waste, and rework. It allows for more predictable output across extended production runs. The adoption of energy-saving extrusion systems and UV-curing technology further contributes to lowering operational costs, aligning with the goal of low-waste cable production.
Flexible Manufacturing For Changing Market Demand
A suitably configured line can manufacture indoor, outdoor, FTTH, armored, ribbon, loose-tube, and tight-buffered cables. The same equipment platform can also support datacom, hybrid, and composite designs with the addition of specific process modules. This adaptability enables manufacturers to respond to shifts in local broadband, data center, and enterprise network demands.
Individual process steps can be installed incrementally, allowing for expansion as orders increase. Modular equipment supports various functionalities, including rollable ribbon, fiber bundling, SZ super-bundling, and final jacketing. These capabilities cater to both high-density data center interconnect cables and standard FTTH products.
Modular upgrades can modernize older lines without necessitating the replacement of every machine. New controls, drives, tension systems, and testing units can extend the service life of equipment and enhance productivity. This strategy safeguards existing investments while pursuing the latest advancements in fiber cable manufacturing technology.
Scalable Solutions For High-Speed Fiber Cable Production
Industrial lines designed for long batches and continuous operation can significantly increase output while maintaining process stability. Automated line synchronization ensures that pay-off, stranding, extrusion, curing, and take-up units operate at a consistent pace. These features are essential for high-speed fiber cable production, facilitating large-scale network deployments.
Effective FTTH cable production solutions involve more than high-speed machinery. They encompass operator training, global installation support, process guidance, and lifetime technical assistance from the supplier. Skilled teams can promptly identify process changes, ensuring reliable production over time.
Scalable machinery helps manufacturers match production capacity and cable quality with future network demand. This alignment provides a practical framework for growth across residential broadband, enterprise systems, and high-density fiber infrastructure.
Conclusion
A modern FTTH Cable Production Line integrates fiber preparation, coloring, secondary coating, buffering, stranding, extrusion, sheathing, testing, and automation into a unified workflow. Each phase ensures stable optical performance, precise dimensions, and reliable cable protection.
The selection of the appropriate setup hinges on cable design, fiber count, materials, adherence to standards, production volume, available factory space, and future expansion plans. Essential components include a fiber coloring machine, a fiber secondary coating line, a tight buffering line, an SZ stranding line, an advanced FTTH cable extrusion line, a fiber cable sheathing line, a fiber ribbon line, and compact fiber unit solutions.
Manufacturers should prioritize controlled fiber tension, dependable materials, automated monitoring, and comprehensive quality testing. Optimal FTTH cable production solutions might encompass single process modules or complete turnkey systems, catering to various cable types such as indoor, outdoor, FTTH, armored, ribbon, and high-density datacom cables.
Employing the correct fiber optic cable manufacturing equipment and efficient production machinery can significantly enhance output while minimizing waste. Scalable, upgradeable systems are instrumental in ensuring reliable broadband deployment, fortifying FTTH network manufacturing, and fostering long-term competitiveness.
Related: Cost Analysis of Implementing a Fiber Secondary Coating Line
How a Fiber Secondary Coating Line Protects Next-Gen Optical Cores
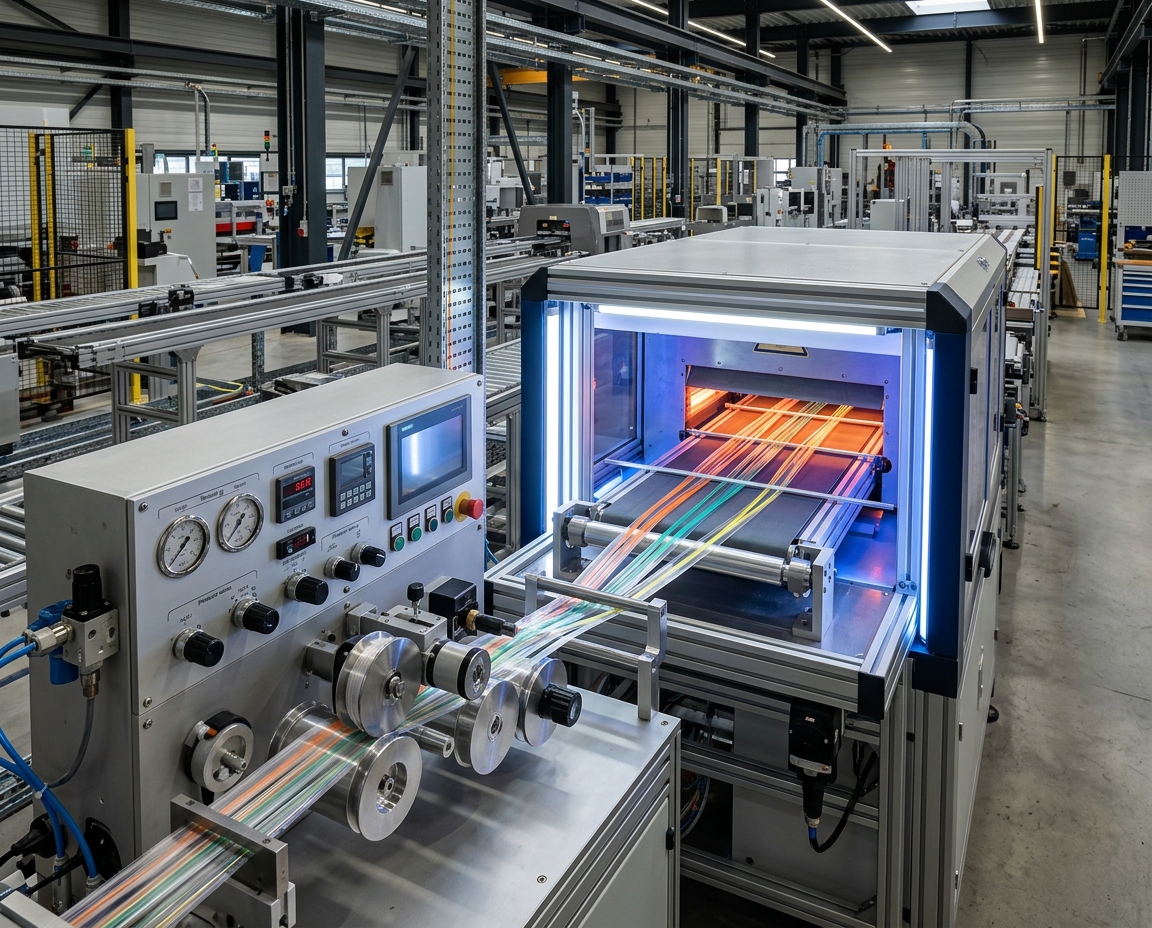 Intermittent Bonded Ribbon Production Line